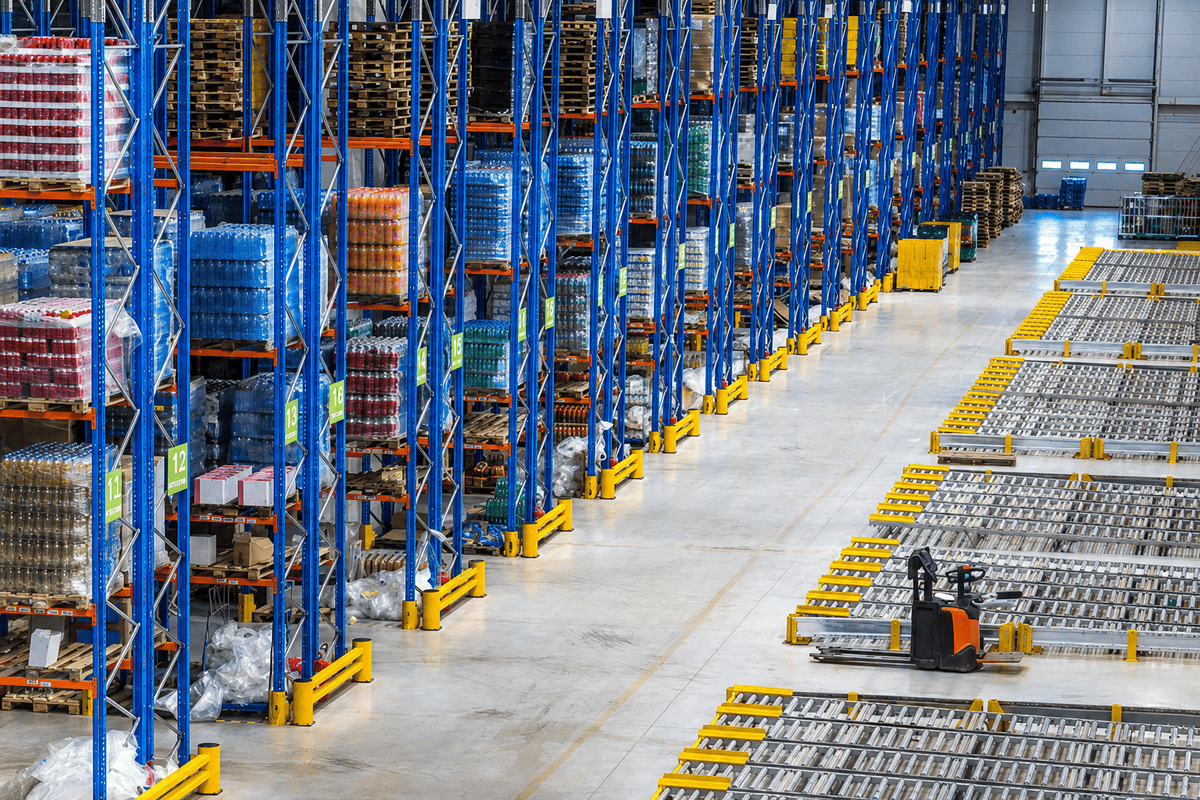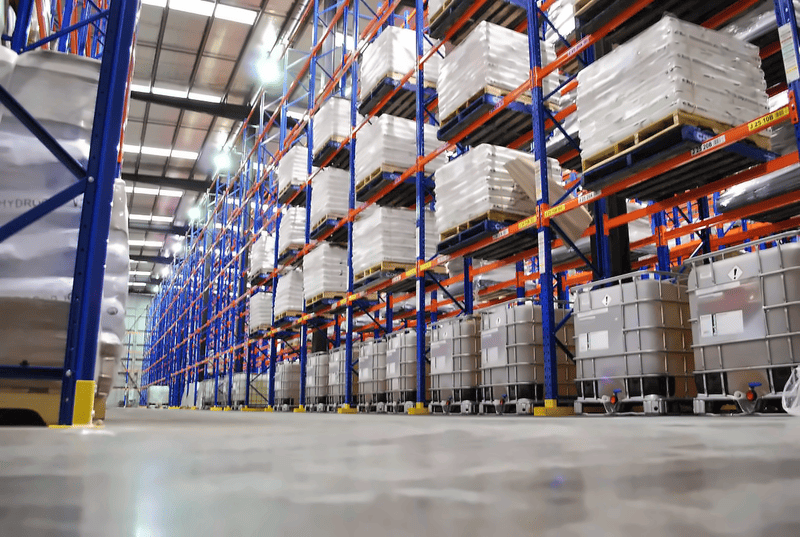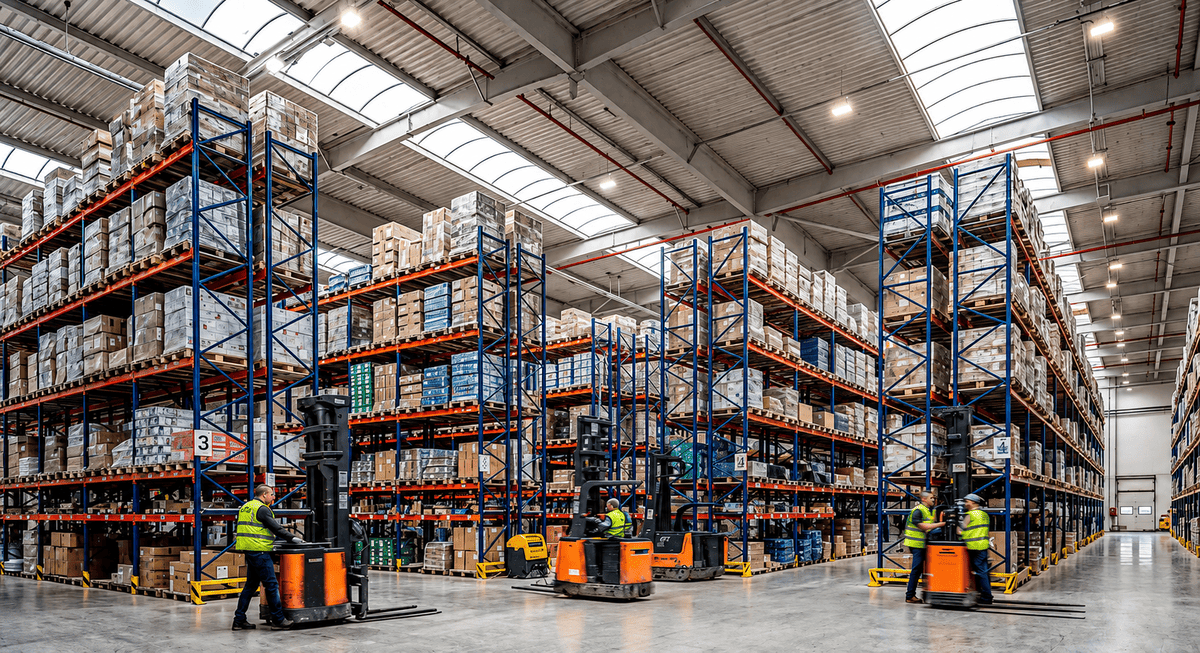


For electronics manufacturers, component distributors and appliance suppliers, storage requirements can vary widely. Small components need organised picking locations, while packaged appliances and finished products may require pallet-based storage. A well-planned electronics warehouse racking layout balances these needs, making inventory easier to manage while protecting products throughout daily operations.
1. Common Storage Challenges in Electronics Warehouses
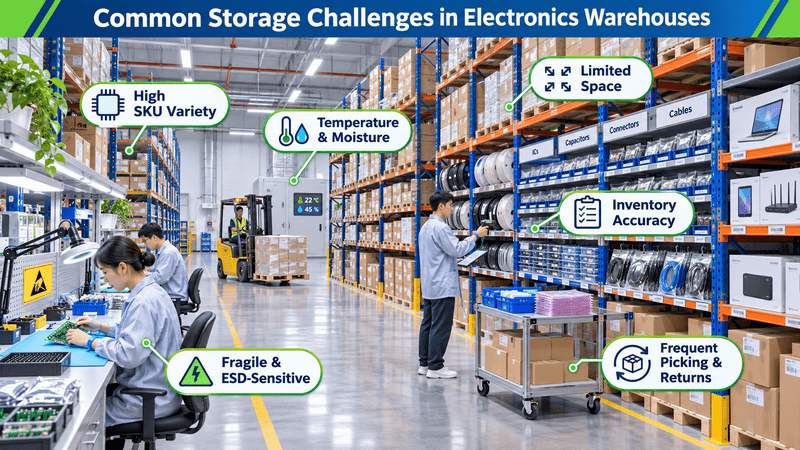
Electronics warehouses face a distinct set of challenges, including high SKU variety, fragile products, electrostatic discharge risks, limited storage space and demanding inventory control requirements. Managing these effectively is essential for keeping products protected, orders accurate and warehouse operations running smoothly.
More racking does not always mean a more efficient warehouse. When components are difficult to locate, valuable products require repeated handling or picking routes become unnecessarily complicated, additional storage capacity can create new problems rather than solve existing ones.
The main challenges include:
- High SKU variety and small components: Electronics warehouses often manage everything from circuit boards and connectors to cables, accessories and finished devices. Many items look similar but have different specifications, making accurate identification and organised storage especially important.
- Fragile and ESD-sensitive products: Sensitive electronic components can be damaged by physical impacts or electrostatic discharge (ESD). Appropriate packaging, careful handling and designated protected areas help reduce these risks.
- Limited space and mixed storage formats: Pallets, cartons, component reels, trays and small parts all require different storage arrangements. Without a suitable layout, some areas become overcrowded while others remain underused.
- Temperature and moisture sensitivity: Certain components require controlled storage conditions to protect their quality. Excessive humidity, condensation or unsuitable temperatures can create problems, particularly for moisture-sensitive electronic parts.
- Inventory accuracy and product obsolescence: Similar components may differ by part number, specification or production batch. As product models change, poor inventory visibility can leave older stock overlooked or difficult to retrieve.
- Frequent picking, replenishment and returns: Production requirements, customer orders and returned products create constant movement through the warehouse. Inefficient picking routes and poorly organised storage locations can increase handling time and errors.
The first step towards a better layout is understanding where daily operations become difficult. A component distributor handling thousands of SKUs may benefit most from accessible shelving and clearly defined picking zones. A warehouse storing larger quantities of packaged electronics, however, may achieve better space utilisation through higher-density pallet racking.
2. Types of Racking Systems for Electronics Warehouses
Common electronics warehouse storage systems include Selective Pallet Racking, Longspan Shelving, Mezzanine Floor Racking, Double Deep, VNA, Push Back, Pallet Flow, Shuttle Racking and Automated Storage and Retrieval Systems (AS/RS). Each offers different advantages depending on product size, storage volume, access frequency and handling requirements.
Selective Pallet Racking
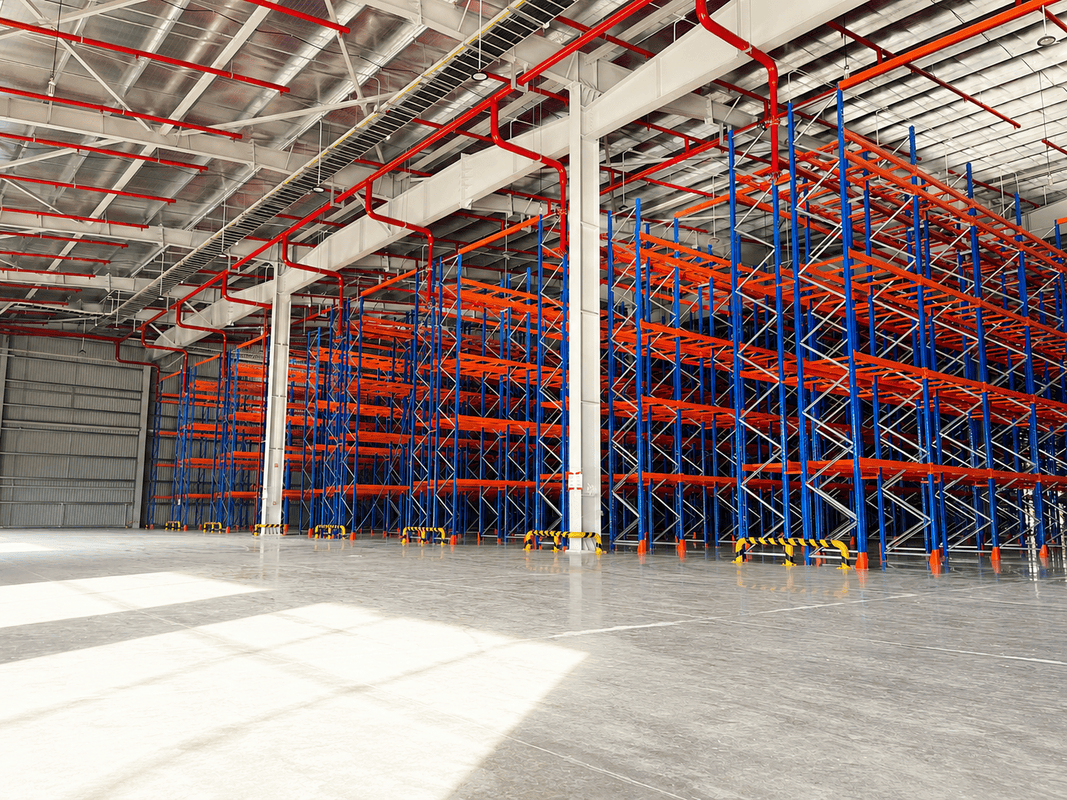
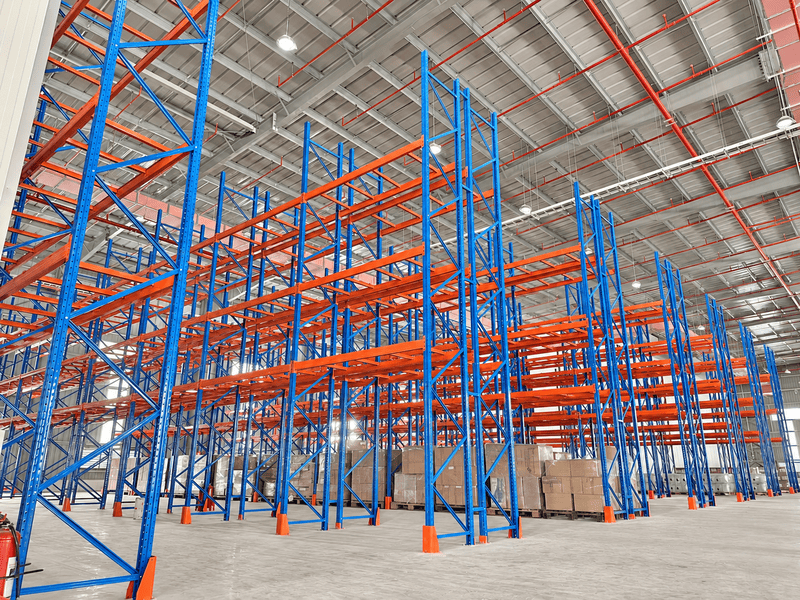
Selective pallet racking provides direct access to individual pallets stored on horizontal beams. Every pallet position can be reached from an operating aisle, allowing warehouse teams to retrieve the required products without moving other loads first.
For electronics warehouses with a broad product range, that flexibility is a major advantage. Different models, product categories and batches can be assigned to clearly identified locations, making stock checks and regular replenishment easier to manage.
- Best for: Electronics distribution centres, appliance warehouses and facilities handling many palletised SKUs.
- Advantages: Direct access to every pallet, straightforward stock identification and flexible storage configurations.
- Consideration: Requires more aisle space than deeper storage systems. Fragile products must also be securely packaged and supported during pallet handling.
Longspan Shelving
Longspan shelving offers practical storage for cartons, small components and manually handled inventory. Adjustable shelf levels accommodate different product sizes, while bins and trays can help keep smaller items separated and easy to identify.
Not every electronics order involves a full pallet. For warehouses regularly picking cables, connectors, accessories or spare parts, longspan shelving can create dedicated picking areas that keep frequently requested products within easy reach.
- Best for: Electronic components, accessories, spare parts, cartons and manual picking operations.
- Advantages: Easy access to smaller products, flexible shelf configurations and organised picking locations.
- Consideration: Shelf load ratings and product support must suit the stored goods. ESD-sensitive components require appropriate protective packaging and handling controls.

Double Deep Racking
Double deep racking stores pallets two positions deep, reducing the number of operating aisles compared with conventional selective racking. A compatible deep-reach truck is used to place and retrieve pallets from the rear positions.
This approach can be particularly useful when several pallets of the same electronic product are held in reserve. It allows more inventory to be stored within the available footprint, although stock allocation needs to account for the reduced accessibility of rear pallets.
- Best for: Bulk electronics, packaged appliances and reserve inventory with multiple pallets per SKU.
- Advantages: Increases storage density while allowing pallet handling from the operating aisle.
- Consideration: Rear pallets cannot be accessed until the front position is clear. Pallet dimensions, packaging stability and retrieval sequences must suit the storage arrangement.
VNA Racking
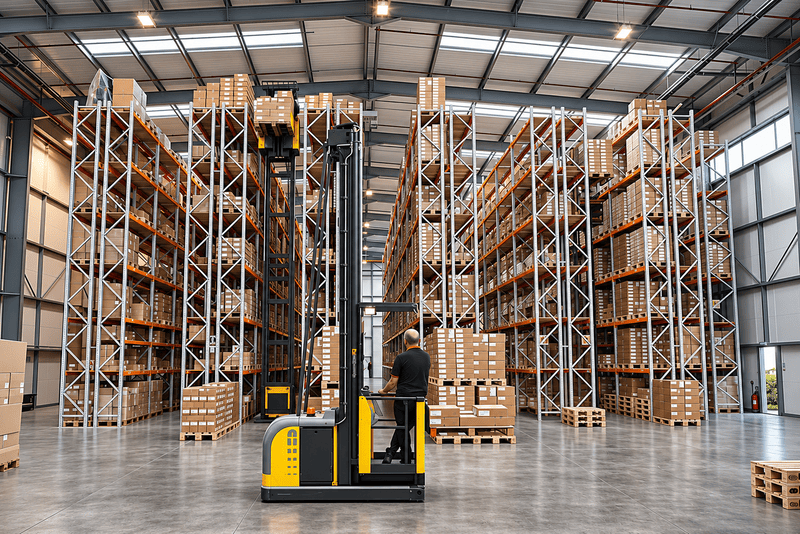
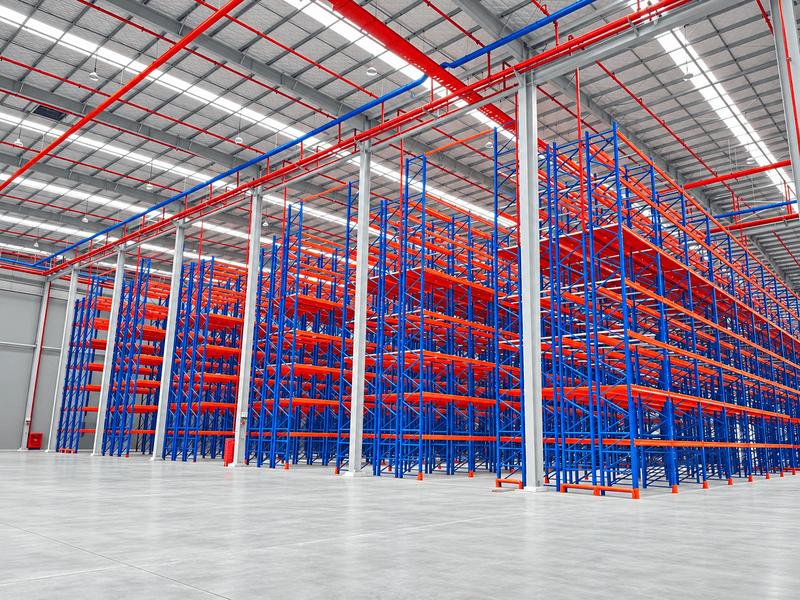
Very narrow aisle (VNA) racking combines direct pallet accessibility with narrower operating aisles. Specialist handling equipment works within reduced clearances, allowing more of the warehouse footprint to be used for storage.
For electronics businesses managing a wide range of products, VNA offers a way to increase pallet capacity without giving up direct access. It can be especially effective in warehouses with high ceilings, where available vertical space has not yet been fully utilised.
- Best for: Electronics warehouses with high SKU variety, limited floor space and sufficient building height.
- Advantages: Improves space utilisation while maintaining direct access to individual pallets.
- Consideration: Requires specialist handling equipment, suitable floor tolerances and careful assessment of operating clearances and load stability.
Push Back Racking
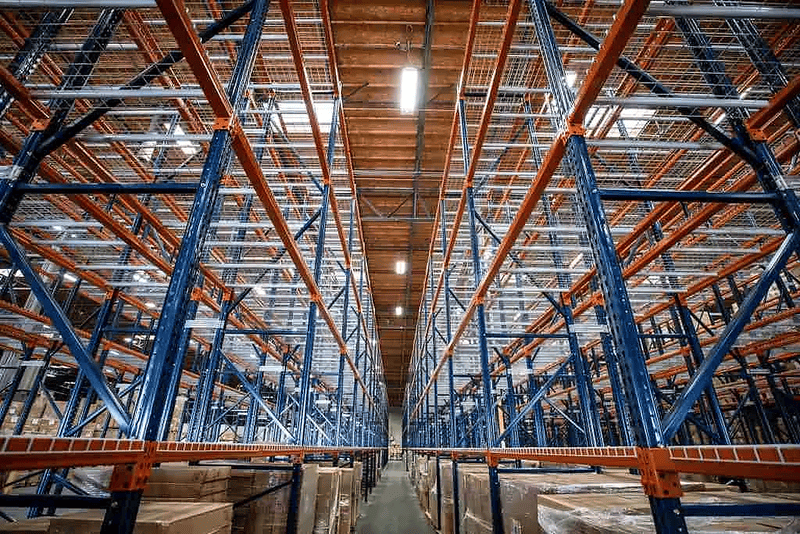
Push back racking stores pallets on moving carts along inclined rails. Loading a new pallet pushes existing pallets further into the lane, while retrieving the front pallet allows the remaining loads to move towards the aisle.
Because loading and retrieval take place from the same working face, the system provides deeper storage without requiring forklifts to enter the racking structure. It can be useful for packaged electronic products held in repeated pallet quantities where last-in, first-out (LIFO) rotation is acceptable.
- Best for: Packaged electronic products, bulk reserve inventory and repeated SKUs without strict FIFO requirements.
- Advantages: Provides high-density storage with pallet handling from a single operating aisle.
- Consideration: Does not support FIFO within an individual lane. Pallet stability, packaging integrity and compatibility with moving components must be assessed.
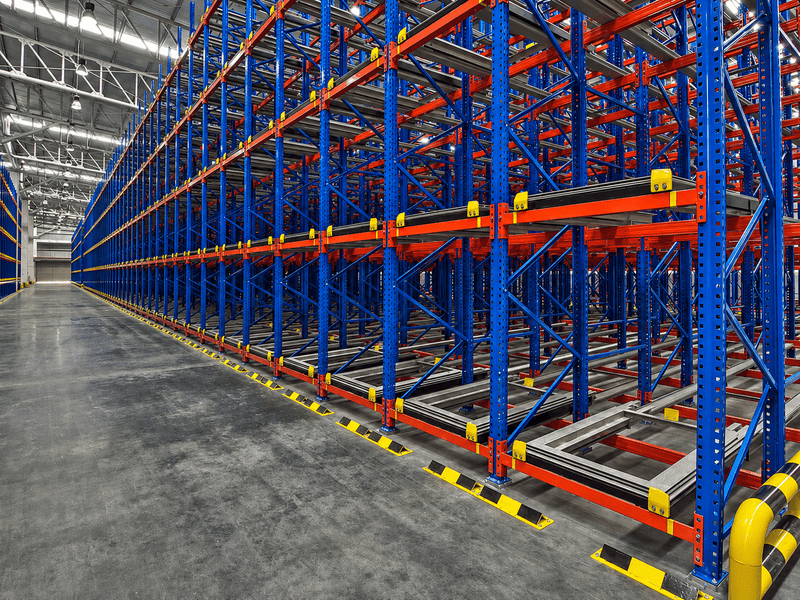
Pallet Flow Racking
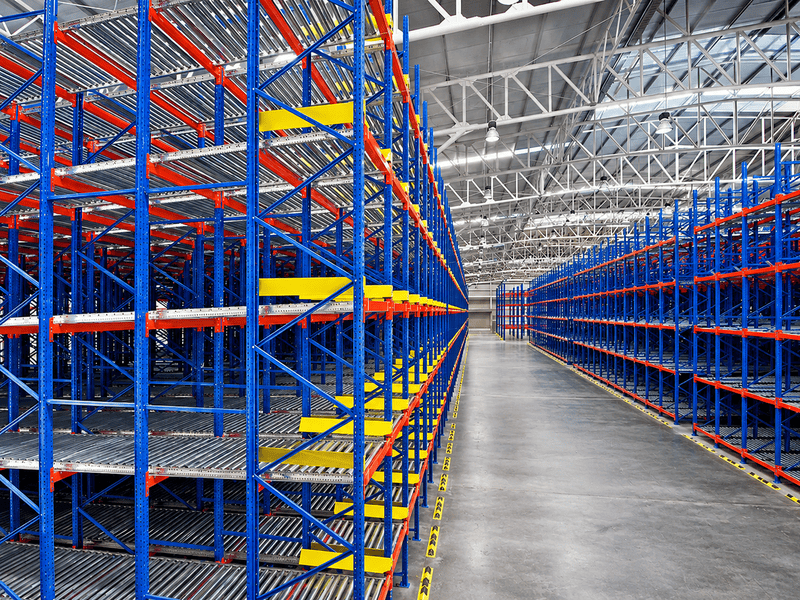
Pallet flow racking uses inclined roller tracks to move pallets from a loading face towards a separate retrieval face. As the front pallet is removed, the remaining loads advance through controlled gravity movement.
This creates a clear stock movement path and supports first-in, first-out (FIFO) rotation. For electronics warehouses handling suitable packaged products, it can help maintain consistent replenishment and retrieval, particularly where inventory age or receiving sequence influences dispatch priorities.
- Best for: Packaged electronic products requiring FIFO movement, regular replenishment and consistent pallet throughput.
- Advantages: Supports FIFO rotation, dense pallet storage and separate loading and retrieval activities.
- Consideration: Requires compatible pallets, stable loads and maintenance of rollers and braking components. Stock allocation procedures must also support the required rotation method.
Shuttle Racking
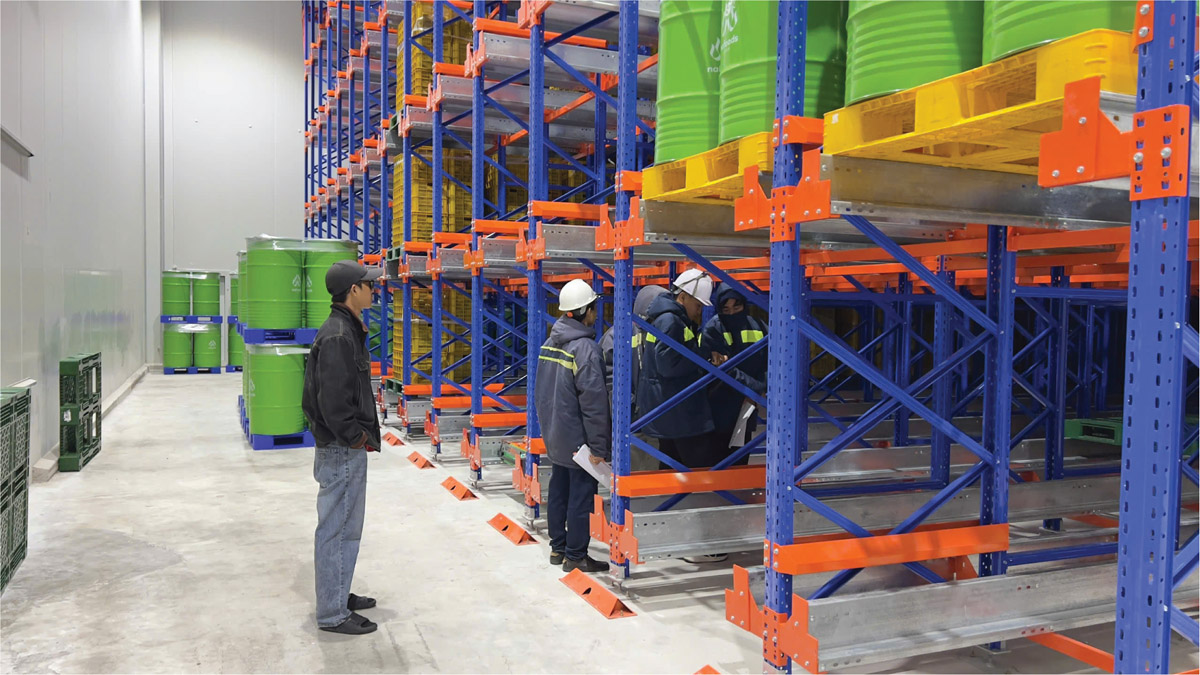
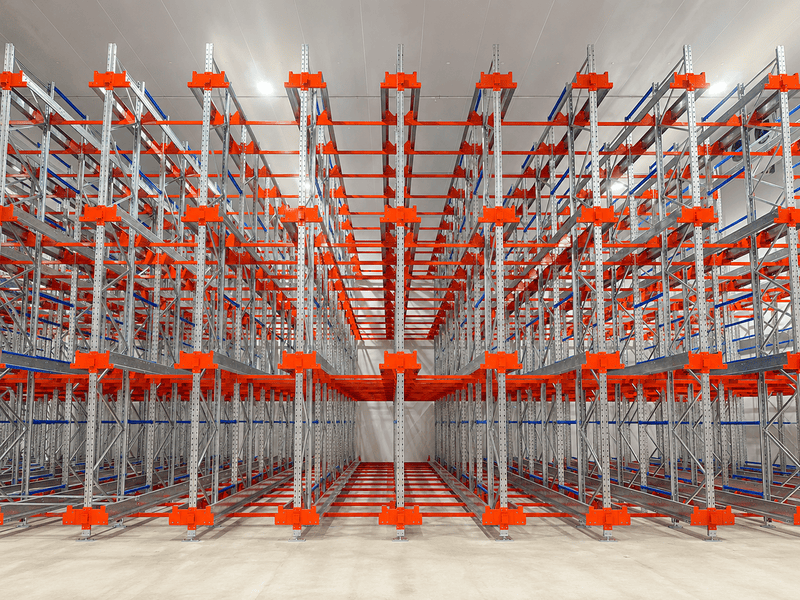
Shuttle racking uses powered shuttles to transport pallets through deep storage channels. Rather than driving into each lane, forklifts typically handle loads at designated transfer points while the shuttle moves pallets to their storage positions.
For electronics distribution centres holding substantial quantities of finished goods, this can provide a useful balance between high storage density and reduced forklift movement. Two-way shuttle systems support deep-lane storage, while four-way configurations can be integrated into more extensively automated operations.
- Best for: High-volume electronics warehouses managing bulk packaged products and multiple pallets per SKU.
- Advantages: Provides high-density storage, reduces forklift entry into storage channels and supports automated pallet movement.
- Consideration: Requires compatible pallets, stable packaging, equipment investment and planning for maintenance, charging and inventory system integration.
Automated Storage and Retrieval Systems (AS/RS)
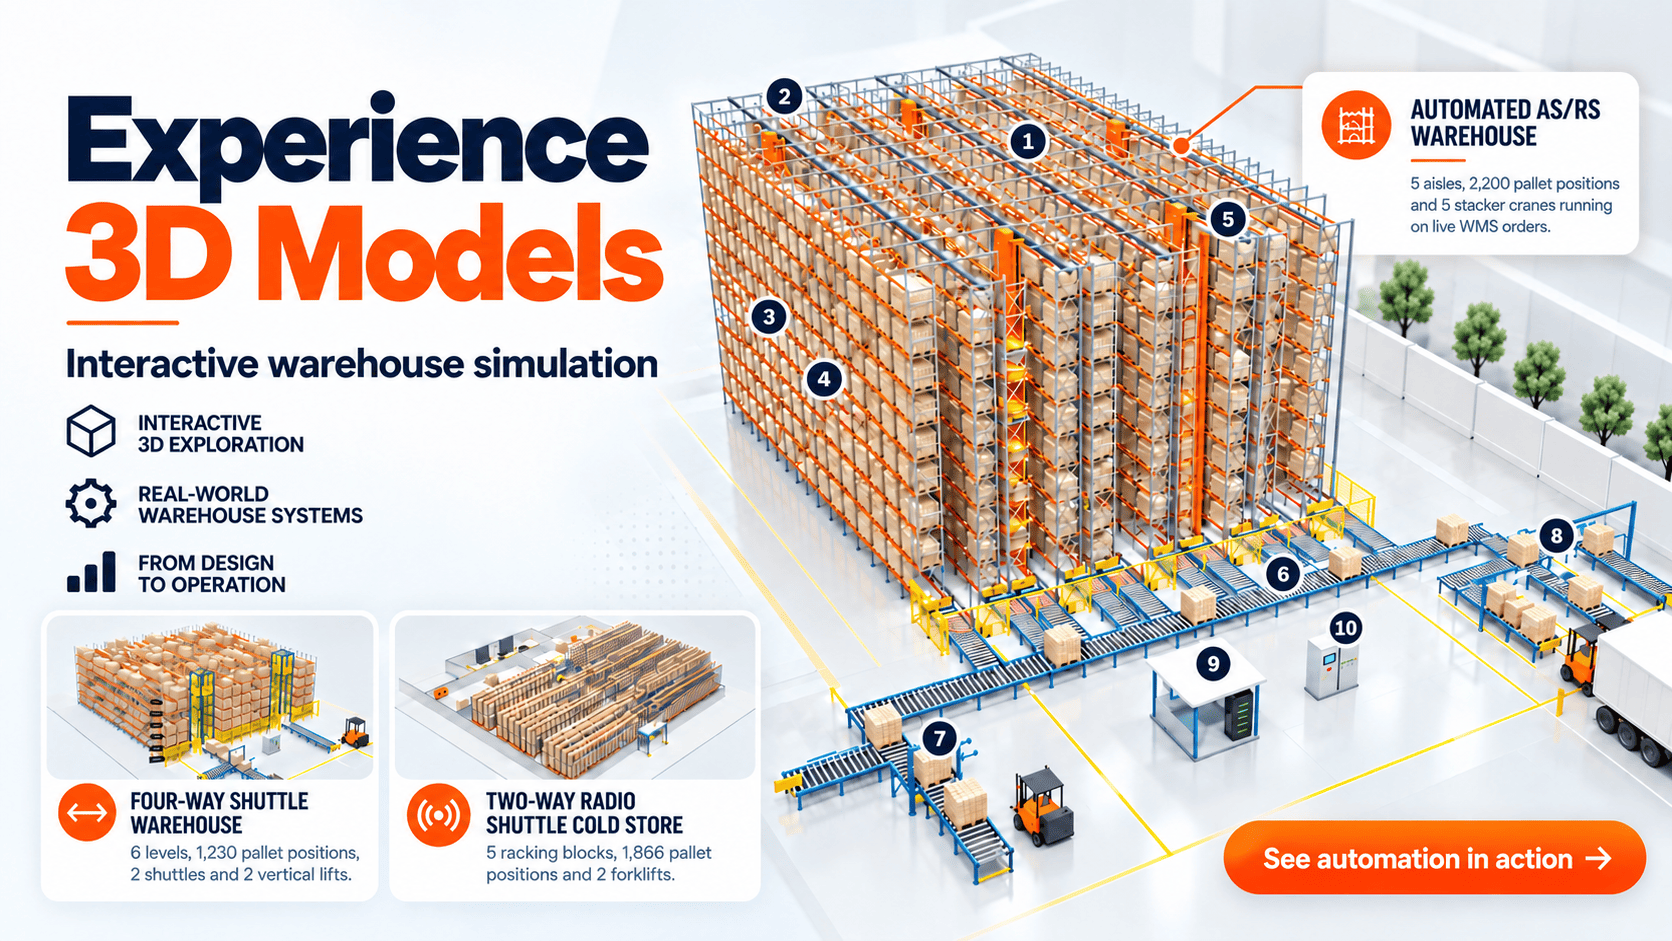
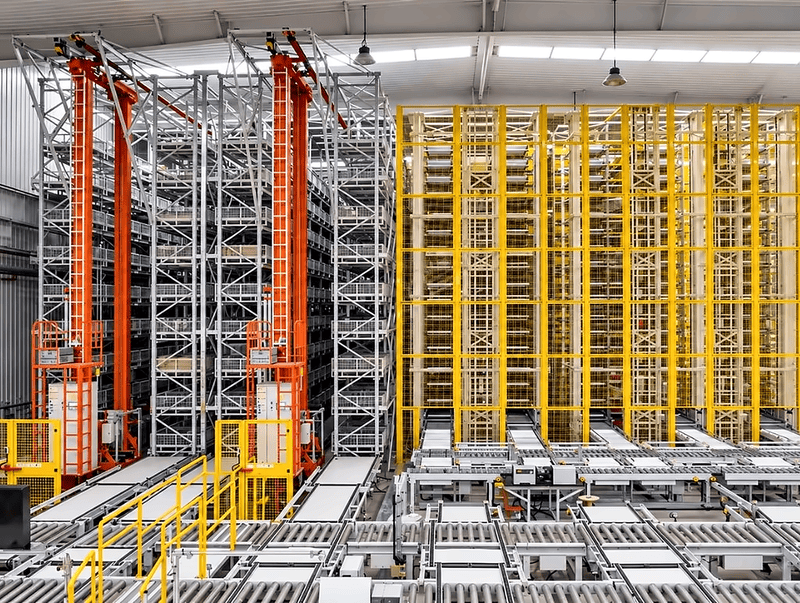
Automated Storage and Retrieval Systems (AS/RS) use computer-controlled equipment to store and retrieve pallets, cartons, bins or other load units. Depending on the configuration, the system may combine stacker cranes, shuttles, conveyors and warehouse control software.
In electronics manufacturing and distribution, automation can be particularly valuable where inventory movements are frequent and accuracy matters. With suitable software integration, it can support consistent product identification, efficient retrieval and improved visibility across storage locations.
- Best for: Large electronics manufacturers, component distribution centres and facilities requiring automated storage and retrieval.
- Advantages: Reduces routine manual handling, supports efficient inventory retrieval and improves stock visibility through integrated control systems.
- Consideration: Requires significant investment, compatible load units, suitable infrastructure and reliable software integration. ESD-sensitive handling must be addressed separately within the overall system design.
3. How to Choose the Right Racking for Your Electronics Warehouse
The right electronics warehouse racking system depends on your product range, packaging formats, picking frequency, available space and handling equipment. Product sensitivity also deserves attention, especially when small components, high-value devices and palletised finished goods are stored within the same facility.
The following table connects common warehouse requirements with systems worth considering:
| Warehouse requirement | Systems to consider | Key selection factor |
| Frequent access across many palletised SKUs | Selective or VNA | Direct pallet access, product variety and replenishment frequency |
| Small electronic components and manual picking | Longspan Shelving | Component dimensions, protective packaging and picking accuracy |
| More capacity for packaged reserve inventory | Double Deep or Push Back | Pallets per SKU, retrieval sequence and packaging stability |
| Limited floor space with diverse products | VNA | Vertical capacity, specialist equipment and direct accessibility |
| FIFO movement for packaged electronics | Pallet Flow | Stock rotation, pallet compatibility and load stability |
| High-volume storage of repeated SKUs | Shuttle | Pallet quantities, storage density and automated handling requirements |
| Automated component or carton retrieval | AS/RS | Load-unit compatibility, picking throughput and software integration |
Consider an electronics distributor managing thousands of small components alongside palletised stock. Longspan shelving may be the most practical choice for frequently picked items, while selective racking can accommodate reserve inventory that needs to remain accessible.
The priorities change when a warehouse holds large quantities of packaged appliances or finished electronics. In that environment, double deep, push back or shuttle systems may provide better storage density, particularly where products are stored in repeated pallet quantities.
Combining different systems is often the more practical solution. A mezzanine can create extra picking space, direct-access racking can accommodate varied products, and higher-density systems can hold suitable bulk inventory without occupying unnecessary aisle space.
Ultimately, the goal is not simply to fit more products into the warehouse. A well-chosen layout should make inventory easier to find, safer to handle and more efficient to move through daily operations.
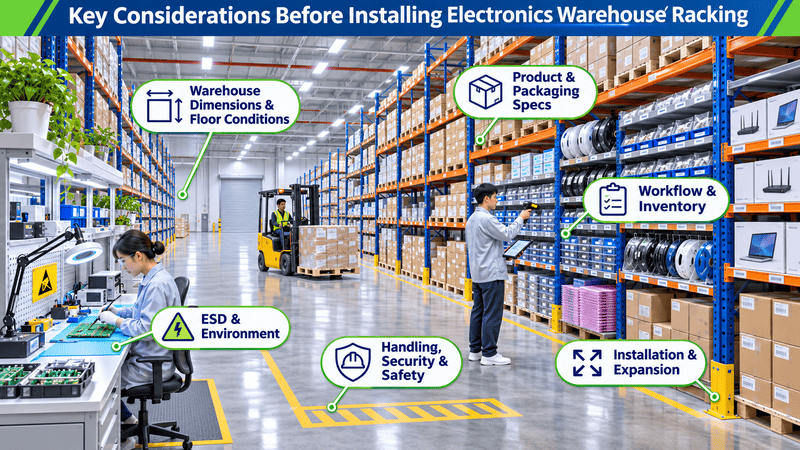
4. Key Considerations Before Installing Electronics Warehouse Racking
Before installing electronics warehouse racking, consider the building layout, product dimensions, ESD protection, environmental conditions, inventory procedures, handling equipment and applicable safety requirements. Looking at these factors together helps avoid a storage layout that offers more capacity but creates difficulties during everyday use.
Warehouse dimensions and floor conditions
Start with an accurate assessment of the usable floor area and clear building height. Columns, doors, building services and operational zones all influence where racking can be installed. Electronics warehouses may also need dedicated space for inspection, testing, packing and returns processing.
The floor slab must be assessed for the proposed rack loads, anchoring and handling equipment. Where VNA or automated systems are planned, floor tolerances and operating conditions become especially important for reliable equipment movement.
Product dimensions and packaging specifications
Electronics inventory comes in many forms, from small component trays and cartons to large appliances and palletised finished goods. Confirm actual product dimensions, loaded pallet weights and packaging characteristics before selecting the storage system.
Fragile products need support arrangements that reduce the risk of crushing, instability or handling damage. Where pallets move along rollers, carts or shuttle channels, their construction and load stability must be compatible with the equipment.
ESD protection and environmental conditions
Electrostatic discharge can damage sensitive electronic components, particularly when products are handled outside their protective packaging. Storage areas should therefore work alongside the facility’s ESD control programme, including suitable packaging, grounding arrangements and designated protected handling areas where required.
Temperature and moisture conditions also need attention. Certain components require specialised dry storage or moisture-controlled packaging to maintain product quality. These requirements should follow manufacturer specifications, and ordinary metal racking should not be assumed to provide ESD protection on its own.
Inventory management and warehouse workflow
Follow the movement of products from receiving and inspection through to storage, picking, packing and dispatch. Identify where frequently requested components should be located and which products can remain in reserve without slowing down daily operations.
Clear location identification is particularly valuable when similar-looking components have different specifications or part numbers. Barcode scanning, serial-number tracking and appropriate inventory procedures can improve stock visibility and help manage product changes over time.
Handling equipment, security and safety
Check forklift dimensions, lifting capacity and turning requirements against the proposed layout. For manual picking areas, consider shelf heights, accessibility and safe handling procedures to reduce unnecessary movement and the risk of product damage.
Racking design should also address applicable Australian safety requirements, including structural capacity, anchoring, load signage, impact protection and inspections. High-value electronics may require restricted-access storage, while lithium battery products need a separate assessment of applicable fire safety, storage and handling requirements.
Installation staging and future expansion
Installing new racking in an operating electronics warehouse requires coordination with production schedules, customer orders and dispatch activities. Temporary stock relocation and restricted work areas should be planned so that essential inventory remains accessible throughout the installation.
Electronics product ranges can change quickly, and today’s storage requirements may look different in a few years. Planning for new SKUs, changing packaging formats or additional automation can make the warehouse more adaptable, provided future modifications are reviewed against the approved racking design.
5. Vinatech Electronics Racking Solutions and Related Projects
Vinatech provides electronics warehouse racking solutions with layout design, supply and installation support. Its 2D and 3D design services help businesses optimise storage capacity, pallet accessibility and warehouse operations.
Selective Pallet Racking for a 7,500 m² Electronics Warehouse
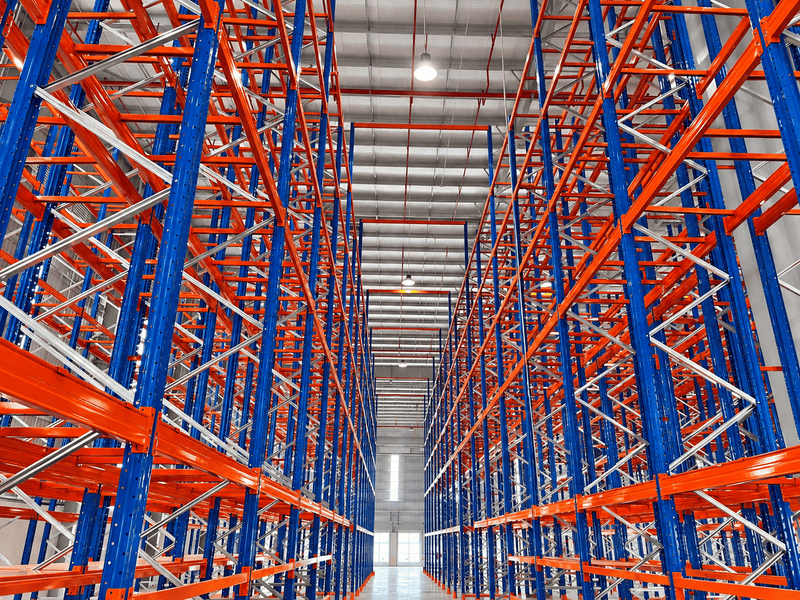
Vinatech delivered a selective pallet racking solution for a 7,500 m² electronics warehouse with a clear height of 10 metres, providing 4,500 pallet positions.
The system provides direct access to individual pallets, supporting efficient storage and handling of electronic components and industrial products. With clearly organised storage locations and accessible operating aisles, the layout helps warehouse teams manage diverse inventory and frequent stock movements.
View the Electronics Selective Pallet Racking Project
Explore related warehouse racking solutions
Explore manufacturing warehouse racking for component and finished goods storage, and e-commerce warehouse racking for layouts that connect reserve stock with order picking.
Start with the challenge that most affects your electronics warehouse: limited storage space, difficult product access, picking errors or inefficient stock movement. A well-planned racking layout can help improve daily operations while keeping valuable inventory organised and accessible.
Contact Vinatech on 0485 083 868 or email info@vinatech.com.au to discuss your electronics warehouse layout, inventory profile and storage requirements.